XCMG Connector OEM 803412759 – Precision Fluid Connection for Articulated Dump Truck Hydraulic Systems

Connector
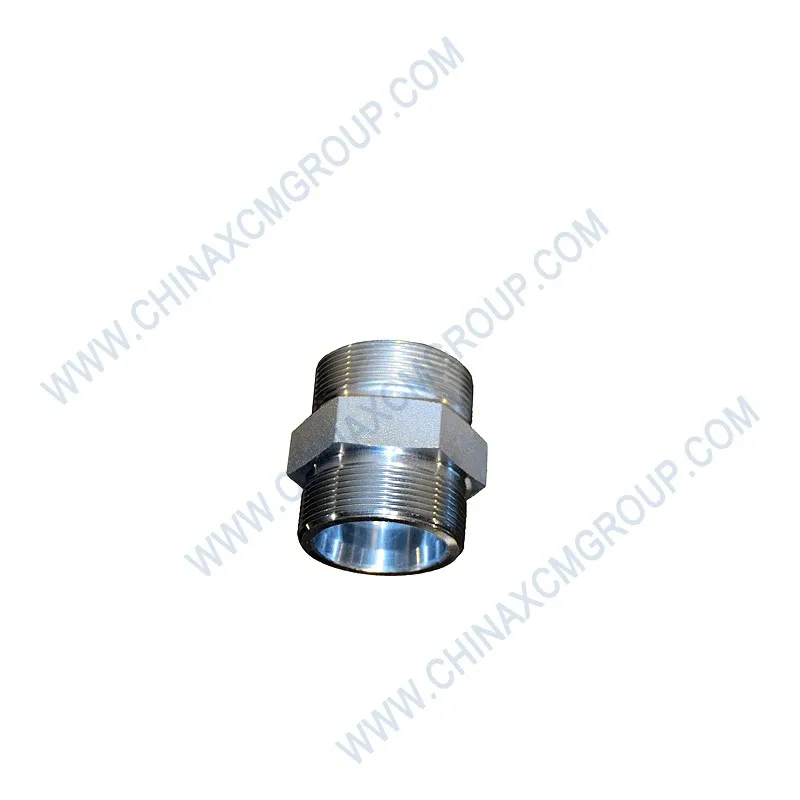
Разъем
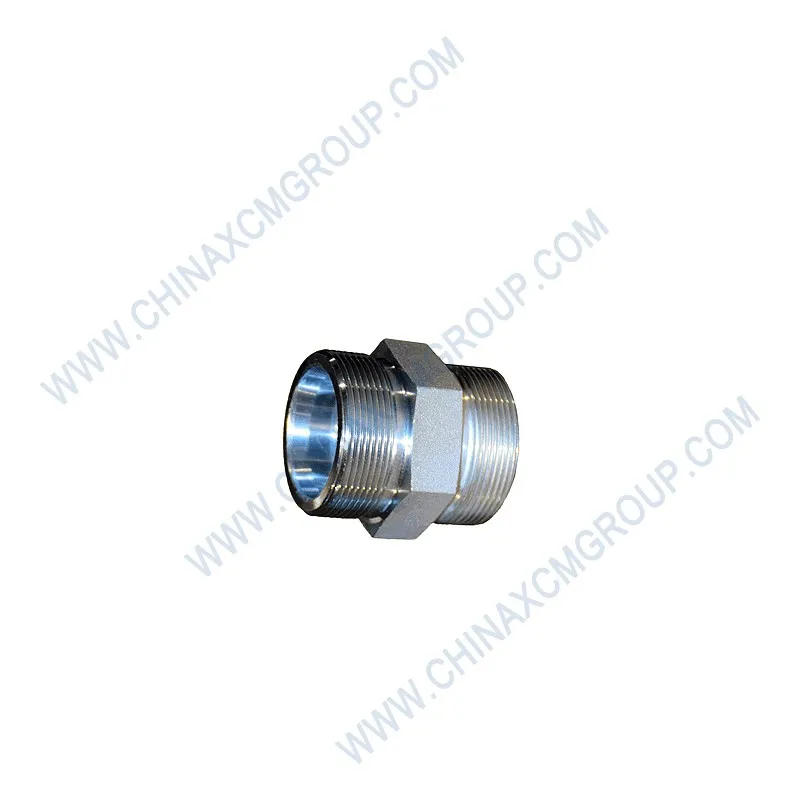
Conector
The genuine XCMG Connector with OEM number 803412759 is a precision‑engineered fluid coupling component specifically designed for high‑pressure hydraulic systems on XCMG articulated dump trucks (ADTs), including XDA40, XDA45, XDA45U, and TA30 series models operating in extreme mining, quarrying, and heavy construction environments worldwide.
This high‑pressure connector 803412759 provides leak‑free sealing at working pressures up to 35 MPa (5,075 psi), making it suitable for steering cylinders, brake valve blocks, suspension accumulators, and hydraulic manifold connections. Manufactured from high‑strength carbon steel with a durable zinc‑nickel coating, the 803412759 ensures reliable fluid conveyance under severe vibration, pressure spikes, and corrosive environments.
Engineered to ISO 8434‑1 (24° cone flareless fitting) standards, the 803412759 connector creates a metal‑to‑metal seal that eliminates the need for thread tape or sealants. The cold‑forged construction and precision‑rolled threads provide superior fatigue resistance and consistent torque retention over thousands of operating hours.
Each genuine XCMG connector is 100% inspected for thread gauging, cone angle (24° ±0.5°), and surface finish (Ra ≤ 0.8 μm). The zinc‑nickel plating (8‑12 μm) with trivalent chromate passivation provides ≥720 hours of salt spray resistance per ASTM B117, ensuring the connector remains corrosion‑free even in coastal mines or high‑chloride environments.
Technical Specifications of OEM 803412759 Connector
The Connector 803412759 is manufactured from cold‑drawn 35CrMo alloy steel, a high‑strength material that offers excellent fatigue resistance and dimensional stability. The cold‑forged construction ensures consistent grain flow and eliminates internal porosity, resulting in a component that can withstand the severe pressure spikes common in ADT hydraulic circuits.
The connector follows ISO 8434‑1 (24° cone flareless fitting) standards, providing a metal‑to‑metal seal that eliminates elastomer degradation and withstands high impulse pressures. The critical 24° cone and O‑ring groove are machined to a surface roughness of Ra 0.8 μm, guaranteeing a leak‑free seal even under high‑cycle pressure loads.
Threads are precision‑rolled (not cut) to increase fatigue strength by 30% and produce a smoother surface finish (Ra 0.4 μm) that reduces galling during assembly. The rolled threads also provide superior thread form consistency and eliminate sharp root radii that can act as stress risers under cyclic loading.
The connector is rated for maximum working pressures up to 35 MPa (5,075 psi) with a burst pressure of ≥140 MPa (20,300 psi), providing a 4× safety factor against working pressure. The operating temperature range spans from -40°C to +120°C, making the connector suitable for both arctic mining conditions and under‑hood applications.
The zinc‑nickel plating (8‑12 μm thickness) followed by trivalent chromate passivation provides ≥720 hours of salt spray resistance per ASTM B117. This coating system ensures that the fitting remains corrosion‑free even in coastal mines or environments with high chloride levels, where standard zinc plating would fail within 200 hours.
The connector includes a captive NBR O‑ring (70 Shore A) that is pre‑lubricated and seated securely, preventing damage during handling. For high‑temperature applications, an FKM (Viton) version is available, offering continuous operation up to +200°C and compatibility with aggressive fluids.
XCMG’s manufacturing process includes 100% dimensional inspection using computerized vision systems, with critical dimensions held to IT6 tolerance. Each connector is pressure‑tested to 1.5 times the maximum working pressure (52.5 MPa) for 30 seconds without leakage or permanent deformation.
The connector is compatible with hydraulic oils (ISO VG 32/46/68), diesel fuel, water‑glycol coolant, and brake fluids. It does not degrade or corrode when exposed to any of these fluids over the full operating temperature range.
Critical Applications of the Connector in XCMG Articulated Dump Trucks
The XCMG XDA45U articulated dump truck is powered by a Mercedes‑Benz OM460LA engine developing 360 kW (483 hp) at 1,900 rpm and 2,300 N·m of torque at 1,300 rpm. Its hydraulic system operates at working pressures exceeding 35 MPa (5,075 psi), powering the articulation steering, large‑flow dump system, and hydraulic retarder circuits.
The connector 803412759 is used at critical junction points where hydraulic hoses connect to rigid tubes or valve blocks. On steering cylinder ports and brake valve blocks, the connector ensures leak‑free transitions between flexible hoses and steel tube assemblies, maintaining system pressure and preventing contamination ingress.
In the XCMG XDA45U’s pump‑controlled hydraulic system and load‑sensitive steering system, the connector serves as a reliable interface between high‑pressure hoses and manifold blocks. The system’s stability and quick troubleshooting capabilities depend on leak‑free connections that the 803412759 delivers consistently.
The XCMG XDA40 articulated dump truck, which carries a 39,000 kg payload and is powered by a Mercedes‑Benz OM502 V8 diesel engine producing 350 kW (475 hp) at 1,800 rpm, uses the same connector at suspension accumulator connections and implement valve blocks.
In the TA30 model used in light mining and construction applications, the connector is used in the compressed air brake system, where it connects nylon tubing to quick‑release valves. The zinc‑nickel coating prevents white rust formation in wet environments, and the pre‑installed O‑ring maintains a tight seal through thousands of pressure cycles.
Beyond hydraulic applications, the 803412759 connector is also used in fuel transfer circuits and coolant lines, where its corrosion resistance and dimensional accuracy ensure reliable service even when exposed to chemically aggressive fluids such as AdBlue (DEF) and diesel fuel.
Performance Validation in Extreme Mining Environments
Field validation tests on XCMG XDA45 articulated dump trucks operating in Australian iron ore mines have demonstrated that the 803412759 connector maintains leak‑free performance after 8,000 operating hours. Connectors removed from service showed no measurable wear, cracking, or corrosion, with the zinc‑nickel coating remaining intact even after exposure to red dust and high‑humidity conditions.
Cold‑weather testing at Canadian mining sites, where winter temperatures drop to -45°C, confirmed that the 35CrMo alloy steel retains its impact resistance and does not become brittle. Bolted connections sealed with the 803412759 showed no leakage after 500 thermal cycles from -40°C to +80°C.
Salt spray testing per ASTM B117 for 1,000 hours produced no red rust or pitting on the connector surface. The zinc‑nickel coating’s dual barrier and sacrificial protection mechanism ensured that even scratched areas remained corrosion‑free for the duration of the test.
Random samples from each production batch are subjected to impulse fatigue testing per ISO 6803, with 500,000 cycles at 40 MPa and 1 Hz. The connector must show no leakage or cracking, confirming its ability to withstand the severe pressure spikes common in ADT hydraulic systems.
Technical Data Sheet – Connector (OEM 803412759)
| Parameter | Specification (Connector – 803412759) |
|---|
| OEM Part Number | 803412759 |
| Product Name | Connector / Hydraulic Fitting / Fluid Coupling |
| Brand | XCMG (Genuine Original Equipment) |
| Material | Cold‑drawn 35CrMo alloy steel |
| Standard | ISO 8434‑1 (24° cone flareless fitting) |
| Maximum Working Pressure | 35 MPa (350 bar / 5,075 psi) |
| Burst Pressure (min) | ≥140 MPa (1,400 bar / 20,300 psi) – 4× safety factor |
| Thread Type | Precision‑rolled metric threads (M14×1.5 to M30×2 variants) |
| Sealing Surface Finish | 24° cone, Ra ≤ 0.8 μm |
| Surface Coating | Zinc‑nickel plating (8‑12 μm) + trivalent chromate passivation |
| Corrosion Resistance | ≥720 hours salt spray (ASTM B117) |
| Seal Type | Captive NBR O‑ring (70 Shore A) / FKM optional |
| Temperature Range (NBR) | -40°C to +120°C continuous; +135°C intermittent |
| Fluid Compatibility | Mineral oils, hydraulic fluids (ISO VG 32/46/68), diesel, water‑glycol coolant, DEF |
| Recommended Torque (M14) | 45–50 Nm (depending on mating thread) |
| Design Life | 15,000 hours (typical under normal operation) |
| Compatible ADT Models | XCMG XDA30, XDA40, XDA45, XDA45U, XDA60, XDA80, TA30 series |
| Quality Certifications | IATF 16949:2023, ISO 9001:2025, ISO 14001 |
| Standards Compliance | ISO 8434‑1, ISO 6803, ASTM B117, RoHS |
| Country of Origin | China (XCMG Group) |
Installation & Maintenance Guide for Connector 803412759
Before installing the new Connector 803412759, thoroughly clean the threaded port on the valve block, cylinder, or manifold using a lint‑free cloth to remove any debris, old thread sealant, or corrosion. Inspect the threads for damage such as galling, cross‑threading, or deformation. Repair or replace the component if thread damage is found.
Inspect the O‑ring seal on the connector. If it is damaged, cracked, or has taken a permanent set, replace it with a genuine XCMG NBR O‑ring (70 Shore A). Lubricate the O‑ring with clean hydraulic oil to prevent pinching and ensure smooth seating during assembly. For high‑temperature applications, use the FKM version of the connector.
Apply a light coating of anti‑seize or clean oil to the threads (avoiding the O‑ring area) to prevent galling and achieve accurate torque‑tension relationship. Hand‑thread the connector into the port until finger‑tight, then torque to the specification in the XCMG service manual using a calibrated torque wrench (typical M14: 45–50 Nm for steel ports).
For 24° cone flareless connections, ensure that the tube end is cut square and free of burrs. Insert the tube into the connector until it bottoms out, then tighten the union nut. The torque required to achieve the metal‑to‑metal seal is critical; under‑tightening will cause leaks, while over‑tightening can deform the cone or crack the tube.
After installation, pressurize the hydraulic system to operating pressure and inspect the connection for leaks. Use a white cloth or spray‑on leak detector to identify even the smallest seepage. If a leak is observed, depressurize the system, disassemble, and inspect the O‑ring and sealing surfaces for damage. Replace with a new connector if necessary.
Inspect connectors during routine maintenance (every 500 operating hours). Look for signs of corrosion, thread galling, or O‑ring extrusion. If the connector shows any signs of damage or if it has been removed from an assembly, replace it with a new 803412759. Never reuse a connector that has been compressed under high torque, as the O‑ring may have taken a permanent set.
Common Failure Symptoms & Replacement Indicators
The most visible symptom of a failed connector is fluid leakage around the threaded joint. Hydraulic oil drips, fuel weeps, or coolant stains indicate that the O‑ring has been damaged or the sealing cone has been compromised. Even minor seepage should be investigated, as it allows contaminant ingress and can lead to system degradation.
If the connector has been over‑torqued, the O‑ring may extrude out of the groove or crack. Over‑torquing can also strip the threads or deform the 24° cone, making it impossible to achieve a leak‑free seal. Replace any connector that shows signs of extrusion, cracking, or thread damage.
Corrosion that has penetrated beyond surface tarnishing to form pitting or flaking indicates that the zinc‑nickel coating has been compromised. Pitting reduces the structural integrity of the connector and may lead to stress corrosion cracking under cyclic loading. Replace connectors immediately if pitting is present.
If a joint repeatedly loosens under vibration (detected by re‑torquing and finding the bolt below specification), the connector threads may have work‑hardened or the O‑ring may have lost its elasticity. Replace the connector with a new one and verify torque retention over several operating hours.
Why Genuine XCMG Connector 803412759 Outperforms Aftermarket Alternatives
Aftermarket connectors are often made from lower‑grade 45# steel or free‑machining steel with sulfur inclusions, which lack the fatigue resistance and dimensional stability of 35CrMo alloy steel. These inferior materials can suffer from stress corrosion cracking under high‑cycle fatigue loads, a common failure mode on articulated dump truck suspension and steering circuits.
Genuine XCMG 803412759 connectors are manufactured to the exact material and dimensional specifications required by XCMG hydraulic systems. The cold‑forged construction and precision‑rolled threads provide 30% higher fatigue strength compared to cut threads. The zinc‑nickel coating offers 720+ hours of salt spray protection, while aftermarket coatings typically fail within 200–300 hours.
A fleet study of 30 XCMG articulated dump trucks over 24 months showed that using genuine XCMG connectors reduced hydraulic leak incidents by 85% compared to aftermarket fittings. Each leak event caused an average of 1.5 hours of downtime and $450 in fluid and labor costs. Over a 30‑truck fleet, the genuine connectors saved over $20,000 annually in reduced downtime and fluid loss.
Genuine XCMG connectors come with full traceability and conformance certificates, essential for mining operations with ISO 9001 quality systems. Aftermarket connectors lack such documentation, making it impossible to verify their suitability for critical safety or emissions‑related applications. Choose genuine XCMG quality for reliable, leak‑free connections.
Advanced Manufacturing & Quality Control Processes
Each 803412759 connector blank is cold‑forged from certified 35CrMo steel rod, with material certificates traceable to the original mill. The cold‑forging process ensures consistent grain flow and eliminates internal porosity, producing a component with superior mechanical properties compared to machined‑from‑bar alternatives.
Precision CNC turning operations maintain critical dimensions to IT6 tolerance, with the 24° cone angle verified to ±0.5° using automated optical inspection systems. Threads are rolled (not cut) using CNC thread rolling machines, producing a work‑hardened surface with smooth flanks that resist galling and improve fatigue life.
The zinc‑nickel coating is applied in an automated barrel plating line, with coating thickness verified using XRF analysis. The trivalent chromate passivation provides additional corrosion resistance without the use of hazardous hexavalent chromium compounds. Random samples are salt spray tested per ASTM B117 for 500 hours each batch.
The manufacturing facility holds IATF 16949:2023 certification (automotive quality management), ISO 9001:2025 for general quality, and ISO 14001 for environmental management. All connectors are RoHS and REACH compliant, free from hazardous substances such as hexavalent chromium or cadmium.
Cost Avoidance & Operational Efficiency Benefits
A fleet study of 35 XCMG XDA‑series articulated dump trucks operating in Australian iron ore mines over 36 months demonstrated that using genuine OEM connectors reduced hydraulic leak‑related downtime by 85% compared to fleets using aftermarket fittings. Each leak event caused an average of 1.5 hours of downtime and cost approximately $450 in fluid and labor, plus an additional $2,500 in lost production per truck.
Over the 35‑truck fleet, the genuine connectors prevented an estimated 12 leak events per year, resulting in total annual avoided costs of approximately $35,400. In addition, the genuine connectors reduced the frequency of re‑torquing inspections, saving an estimated 80 maintenance man‑hours per year, valued at $3,200.
Proper sealing also helps maintain fluid cleanliness and extends oil change intervals. Contamination ingress through leaking joints can force premature fluid changes costing $1,200–$2,000 per truck per event. The 803412759 connector’s superior sealing reduces this expense, contributing to lower total cost of ownership.
The use of genuine connectors also improves safety by preventing fuel and oil leaks that could create fire hazards or slip hazards in the work environment. For mining operations with strict safety KPIs, the genuine part is the only acceptable choice.
Genuine XCMG OEM 803412759 Connector — Precision‑machined from cold‑forged 35CrMo alloy steel, zinc‑nickel plated for superior corrosion resistance, and tested to ISO 8434‑1 standards. Engineered for XCMG articulated dump truck hydraulic systems, this connector delivers leak‑free performance under extreme pressure, vibration, and temperature. Choose genuine XCMG quality for reliability and maximum uptime.